In the medical sector and life sciences, identification is not a logistics side issue, but a critical part of patient safety. In the processing of blood, cells and tissues (Medical Products of Human Origin, MPHO), the international ISBT 128 standard is the norm. But how do you translate these complex rules into a workable, error-free and efficient digital process?
At Giesbus Labeling Solutions we support healthcare institutions and laboratories in designing labeling systems that not only comply with the rules, but also reduce operational pressure.
What is the challenge with ISBT 128?
The ISBT 128 standard is designed for global traceability. This brings specific technical challenges:
- Unique identification: correctly generating and printing Donation Identification Numbers (DIN).
- Complex data structures: using 2D Data Matrix symbols for compound messages (several data points in one scan).
- Traceability: a closed chain from donor to recipient, with every step logged.
Many institutions still work with outdated systems or partly manual processes. This considerably increases the risk of human error.
The solution: central label management with Loftware NiceLabel
In our recent healthcare projects we use the Loftware NiceLabel LMS (Label Management System). This platform acts as the central brain of the labeling infrastructure.
- 1. Direct database integration (the single source of truth)
By connecting NiceLabel directly to the clinical SQL database, we eliminate manual data entry. The information on the label always mirrors the data in the clinical system one-to-one. We configure the logic so that variables such as expiry dates, product codes and split codes are mapped automatically. - 2. GxP and FDA compliance
In a regulated environment an audit trail is mandatory. The LMS offers a digital document management system (DMS) with version control and electronic signatures. Every change to a label design is logged: who changed what, and who approved it? - 3. User-friendly HMIs for the shop floor
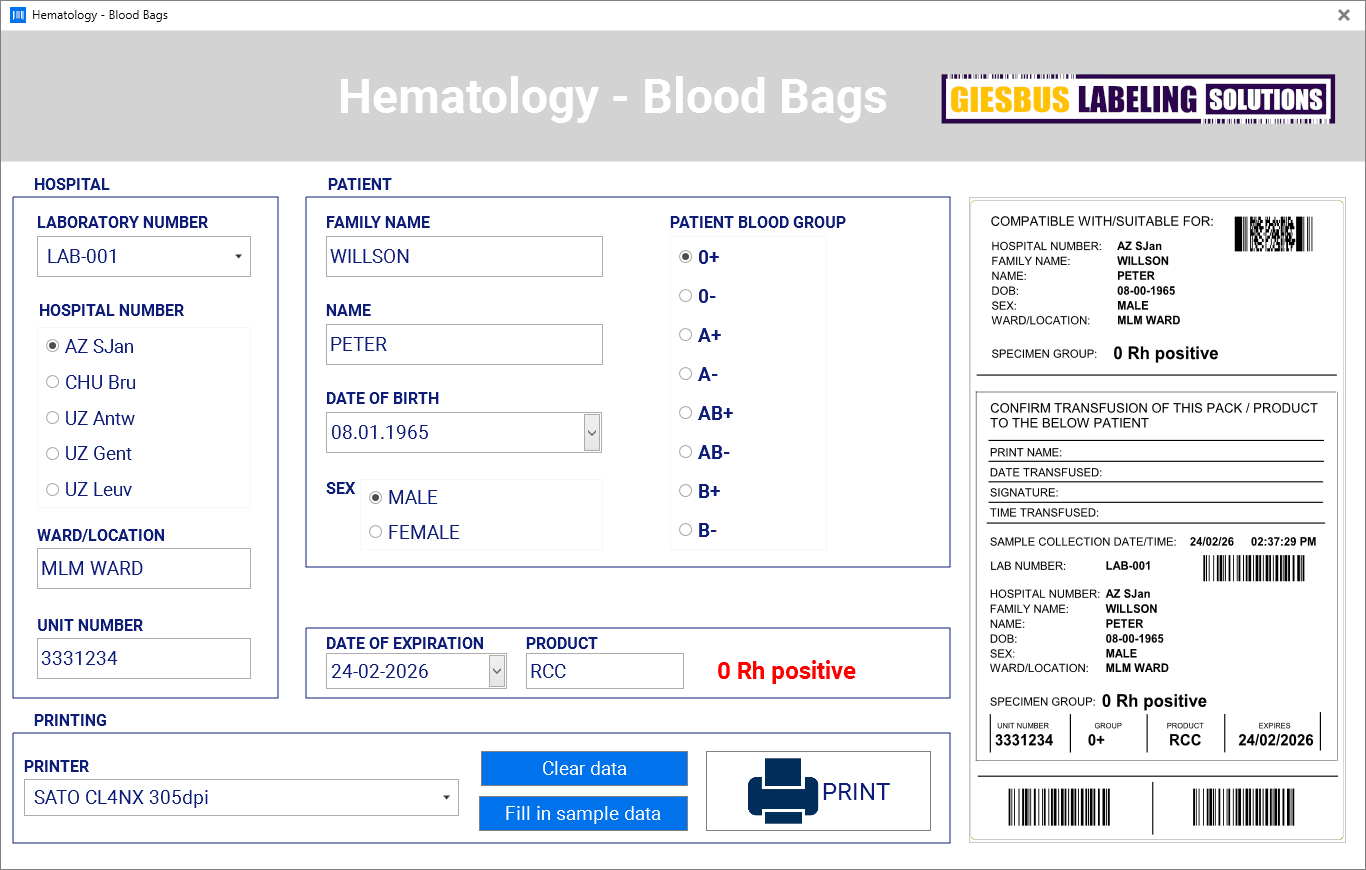
We develop tailor-made print screens (PowerForms) for medical staff. Operators only see the fields they need and often only have to scan an order number. The software does the rest. This increases speed and minimises distraction.
Result: operational excellence
The technical realisation of a modern labeling system brings calm to the organisation. The benefits at a glance:
- Zero error margin: automation removes the human factor from data transfer.
- Audit-ready: always meet the requirements of inspections and regulators.
- Scalability: new standards or sites can easily be rolled out centrally.
Conclusion
Implementing ISBT 128 is a complex project that requires in-depth knowledge of both the standard and the IT infrastructure. Giesbus combines years of experience with the power of Loftware NiceLabel to make this transition seamless. Also read whether NiceLabel/Loftware is suitable for a pharmaceutical GMP environment.
Would you like to know more about our approach to medical labeling, or see a no-obligation demo of the LMS platform? Contact our specialists.
Contact us for more information →
Prefer to look for yourself first? Take the free Labeling Compliance Scan or use the ROI calculator to see what your labeling costs today.
More information about the standard?
Visit the official ICCBBA website for the latest updates on MPHO identification.
 Vrieswijk 27
 +31 72 533 2998

 Chamber of Commerce 86756850
 Loftware Cloud Solutions Expert